Flexible intralogistics: Fluro revolutionizes warehousing and production
Xpert Pre-Release

Available in 27 languages 📢
Prefer Xpert.Digital on GoogleⓘPublished on: October 3, 2026 / Updated on: October 3, 2026 – Author: Konrad Wolfenstein
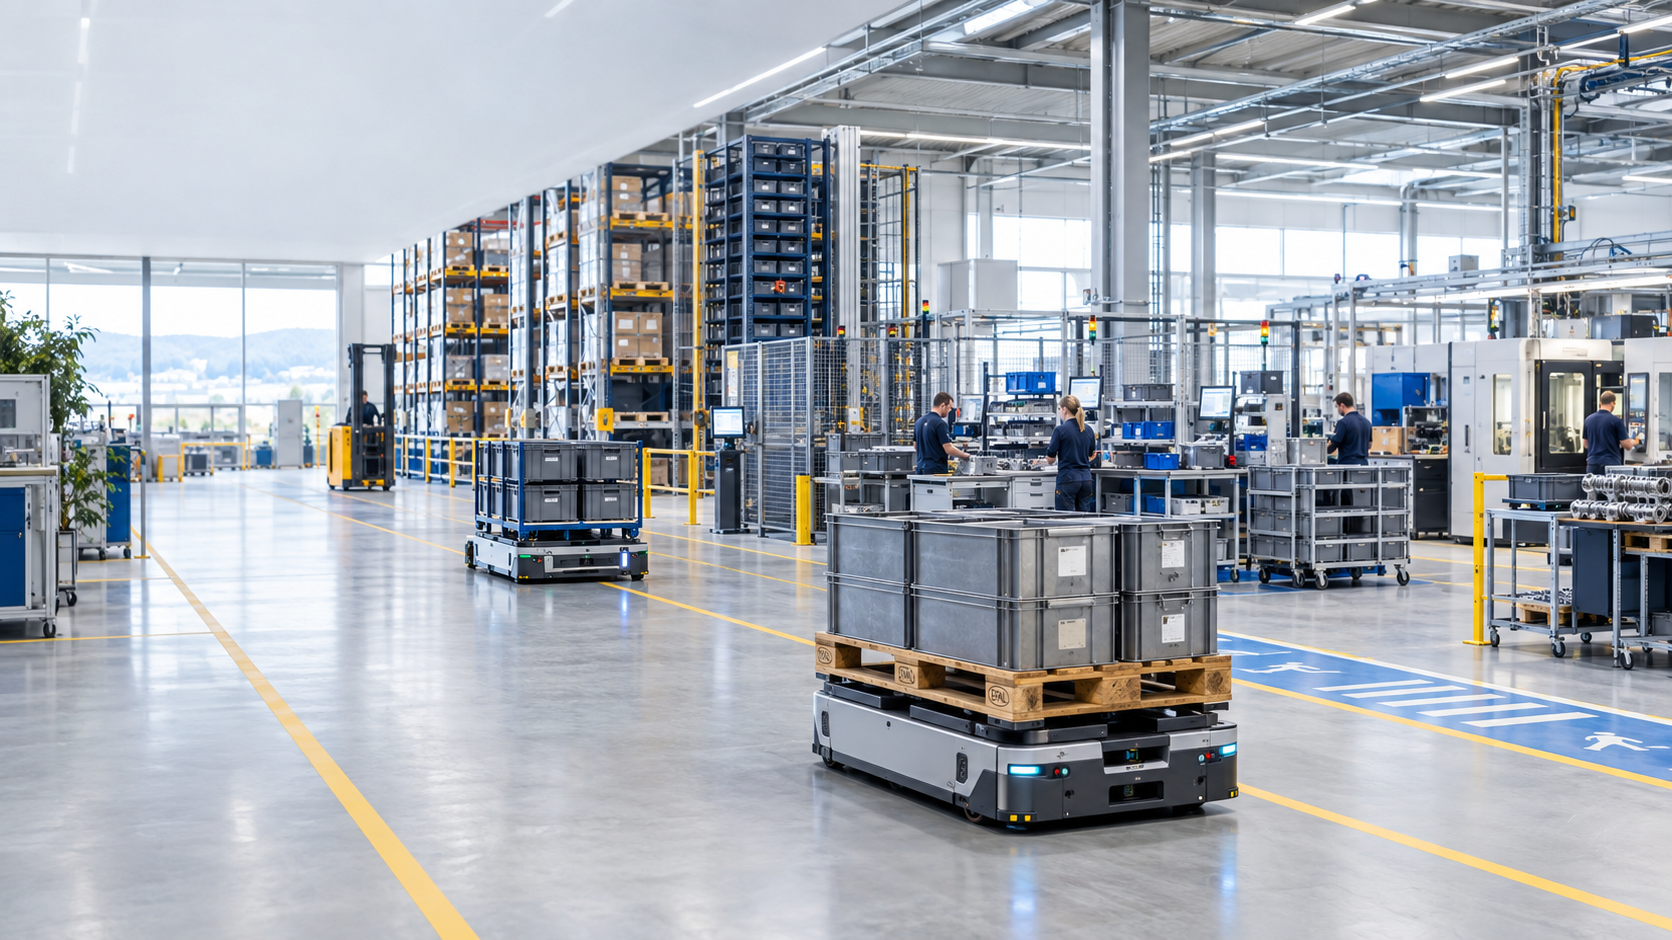
Flexible intralogistics: Fluro revolutionizes warehousing and production – creative image on the topic, with AI: Xpert.Digital
Mobile robots in SMEs: Smarter automation instead of bigger
Growth strategies for medium-sized businesses: Fluro focuses on dynamic intralogistics
Innovative logistics solutions: Fluro is shaping the future of material flow
In the context of advancing automation and digitalization in industry, the medium-sized company Fluro in Rosenfeld has taken a bold step to redesign its warehousing and production processes. The construction of a modern production and logistics hall means far more to Fluro than simply creating additional storage space. Rather, it represents a fundamental review and redesign of existing processes and material flows. Instead of rigid conveyor technology, Fluro is relying on five autonomous mobile robots, which are intended to revolutionize the internal material flow between warehousing, order picking, and production.
This innovative approach reflects the increasing flexibility of intralogistics. Fluro avoids the common reflex of defining automation solely through the use of permanently installed technology, instead focusing on intelligent, adaptable solutions. The planned operational launch in December 2027 marks not only a milestone in the project timeline but also the transition from historically grown structures to data-driven, scalable intralogistics. By integrating a two-aisle pallet warehouse and a shuttle-based small parts warehouse, Fluro will be able to handle diverse requirements and materials more efficiently. In this context, it becomes clear that the future of intralogistics depends not only on technology but also on data quality and process flexibility.
Flexible intralogistics as a growth system: How Fluro reconnects warehouse and production
Five mobile robots instead of rigid conveyor technology – medium-sized businesses are not automating more, but more intelligently
For a medium-sized industrial company, the construction of a new production and logistics hall is far more than just a building project. It necessitates a fundamental review of established processes, inventory levels, routes, and responsibilities. This is precisely where the strategic significance of Fluro's project in Rosenfeld lies. The specialist for spherical plain bearings and rod ends is not merely creating additional storage space, but rather redesigning its internal material flow. Five autonomous mobile robots will transport pallets and containers between the warehouse, order picking, and production. This transport concept is complemented by a two-aisle pallet warehouse, a shuttle-based small parts warehouse, and a warehouse management system that controls the facility and connects it to the ERP system. The planned start of operations in December 2027 therefore marks not only a date on the project calendar, but also the transition from historically grown structures to a data-driven, scalable intralogistics system.
Economically, the decision is remarkable because Fluro doesn't follow the common reflex of equating automation with as much permanently installed technology as possible. Conventional conveyor systems can be extremely efficient with high, stable volumes and consistently identical transport patterns. However, they tie up space, capital, and layout. If machines are relocated, production programs are changed, or material flows are reorganized, additional conversion costs quickly arise. Mobile robots follow a different logic. They shift some functionality from the physical infrastructure to vehicles, sensors, and software. This doesn't automatically make the system cheaper or simpler, but it does increase the number of operational options. The core of the project, therefore, is not the purchase of five vehicles, but rather the acquisition of adaptability.
Growth makes bad roads expensive
Fluro has grown over decades. Founded in 1976, the company has evolved from a local specialist into an internationally operating manufacturer of precision fasteners. With this growth, the product range, order volume, inventory size, and organizational complexity have increased. Especially for a company that offers both standard products and customized solutions, simply creating more storage space is not enough. Varying batch sizes, shifting priorities, and supplying production demand a material flow that is both reliable and responsive.
The existing logistics center had reached its capacity limits. Storage areas were partially decentralized, while stationary conveyor technology occupied valuable space without providing a corresponding benefit everywhere. Such structures are typical in growing medium-sized companies. What made sense in an earlier development phase is gradually superseded by additional products, machinery, and orders. New space is created wherever it happens to be available; intermediate storage compensates for a lack of transparency; employees smooth over system breaks through experience and improvisation. This often works surprisingly well for a long time, but it incurs hidden costs in the form of additional routes, search times, redundant movements, waiting lists, and difficult-to-plan priorities.
These costs rarely appear as a separate line item in the profit and loss statement. They are spread across personnel, space, inventory, energy, error correction, and lost machine productivity. Therefore, the economic pressure often only becomes apparent when capacity limits are reached. At that point, simply adding a few shelves or deploying more forklifts is no longer sufficient. Increased manual transport can even worsen a disorganized system, as additional vehicles and personnel will occupy the same bottlenecks. The new building offers Fluro the opportunity not only to treat symptoms but to completely redesign the spatial and digital architecture of its material flow.
Automation without a concrete corset
The deliberate departure from a predominantly stationary conveyor technology concept is the strategic core of the solution. Fixed roller conveyors, chain conveyors, or transfer lines are by no means obsolete. With clearly defined, high-frequency, and long-term stable connections, they can achieve high throughputs with very good availability. Their disadvantage becomes apparent where sources, sinks, quantities, or load carriers change frequently. Every mechanical system permanently reflects an assumption about future operation. If this assumption later proves incorrect, the efficient connection becomes a barrier.
Autonomous mobile robots decouple the transport task and the route to a greater extent. They orient themselves in their environment, calculate routes dynamically, and can avoid obstacles or choose alternative paths. New transfer points can generally be set up via software with manageable adjustments, as long as the areas, safety distances, load capacities, and process interfaces are suitable. This does not eliminate all infrastructure requirements, however. Mobile systems also need suitable surfaces, reliable wireless networks, defined traffic rules, safe transfer stations, charging points, and a well-thought-out layout. The crucial difference is that a larger part of the system remains reconfigurable.
This reconfigurability has real economic value. It's comparable to an option: The company pays today for the ability to respond to future requirements that are not yet fully known. This is particularly relevant for a specialized manufacturer. Product variants can increase, manufacturing technologies can change, and new markets can demand different batch sizes or delivery times. A rigid system optimizes one expected state. A mobile concept optimizes the ability to manage multiple possible states. In an uncertain industrial environment, this flexibility can be more important than the last theoretical percentage point of maximum throughput.
Five vehicles constitute a system, not a fleet on hand
The five planned autonomous mobile robots constitute a comparatively small fleet. This is a key indicator of the project's logic. The goal is not spectacular full automation with as many vehicles as possible, but rather the targeted automation of recurring transport routes. The robots will handle the material flow between the warehouse, order picking, and production. They will move pallets and, if needed, independently pick up a carrier that can hold up to four containers. This allows the same vehicle base to serve different load carriers and process types.
Multifunctionality improves capacity utilization but simultaneously increases the demands on planning and control. A vehicle that handles both pallets and containers must not only be technically capable of handling both load types. Orders, priorities, transfer heights, load securing, time windows, and return processes must also be compatible. Otherwise, the result may be flexible hardware, but inflexible operations. A particularly important question is how to avoid empty runs and consolidate transport orders. For example, a robot supplying a production area could pick up empty containers, finished parts, or other items on its return journey. The economic benefit arises not from kilometers driven, but from productive transport chains with as few unused movements as possible.
A fleet of five vehicles also offers a degree of redundancy. If one vehicle is temporarily unavailable due to charging, maintenance, or a malfunction, the fleet can redistribute tasks. However, whether the remaining capacity is sufficient to handle all peak demands depends on the specific order profile. Crucial factors are not average values, but rather peak loads, overlaps, and the most critical supply cycles. A sound fleet design must therefore simulate transport requirements, travel times, waiting times, battery concepts, malfunctions, and future growth. Too many vehicles generate unnecessary capital expenditure and traffic; too few make the entire production process vulnerable to delays. The optimal fleet size is thus not simply a manufacturer's specification, but the result of a robust operating model.
The bearing becomes the pace setter
The overall system comprises a two-aisle pallet warehouse and a shuttle-based small parts warehouse. Both warehouse types fulfill different economic functions. The pallet warehouse consolidates larger load units and ensures an organized supply of palletized items or materials. Two aisles limit structural complexity but require careful dimensioning of storage and retrieval capacity. The small parts warehouse, on the other hand, addresses the large number of small items and containers typical for product variety, order picking, and production supply.
Shuttle systems can dynamically store and retrieve containers and are often modularly scalable. Their benefits lie not only in high storage density but also in the ability to provide required items in sequence and with short access times. This dynamic capability is significant for Fluro because precision parts and components must not only be stored but also made available according to orders, assemblies, or production requirements. An automated small parts warehouse can reduce search and walking distances, make inventory more transparent, and decouple order picking from the personal location knowledge of individual employees.
However, the warehouse should not be optimized solely for maximum performance. A shuttle system that provides containers faster than order picking or mobile robots can handle them creates queues instead of increasing productivity. Conversely, insufficient retrieval capacity can slow down production. The key planning metric is therefore end-to-end throughput from the storage location to the point of use. This includes buffers, transfer stations, and priority rules. The most economically efficient system is not the one with the fastest individual components, but rather the one whose components work together effectively within the actual order mix.
Software determines the usefulness of hardware
The UniWare warehouse management system provides overarching control and connects the entire system to Fluro's ERP system. This level is at least as crucial to the project's success as the vehicles, racking, and shuttles. The ERP system is aware of commercial and production-related requirements, orders, and inventory levels. The warehouse management system translates this information into operational warehousing and transportation tasks. It must decide which stock is used, when a container is retrieved, at which transfer point it is ready, and which transportation order receives which priority.
This creates a digital nervous system whose quality directly impacts delivery capability and plant productivity. If master data is faulty, bookings are delayed, or interfaces are unclearly defined, the technology automates not the solution, but the error. An incorrect inventory level won't be corrected by a fast shuttle. A missing load carrier blocks autonomous transport just as much as manual transport. Therefore, implementation must be accompanied by rigorous data cleansing, unambiguous process rules, and clear accountability.
Exception handling deserves special attention. Normal processes are relatively easy to model. However, damaged containers, illegible labels, blocked transfer points, rush orders, quality checks, missing parts, or short-notice production changes are economically critical. A robust system recognizes such situations, prioritizes them, and guides employees clearly through the process. If every deviation requires a specialist, new dependencies arise. Good automation not only reduces manual routine but also makes disruptions visible, traceable, and manageable.
The market is growing despite a weak economy
The project coincides with a contradictory market phase. On the one hand, the German materials handling and intralogistics sector is under economic pressure. After a production volume of around €27.7 billion in 2024, output declined significantly in 2025; stagnation was largely expected for 2026. Weak investment in key industrial sectors, lower exports, and geopolitical uncertainty are weighing on suppliers. This decline demonstrates that automation growth is not independent of the overall industrial economy.
On the other hand, mobile robotics is developing dynamically in terms of its structure. Worldwide, around 102,900 robots for transport and logistics tasks were sold in 2024, 14 percent more than in the previous year. Approximately 81,800 of these were mobile robots for intralogistics applications. Transport and logistics thus accounted for more than half of the market for professional service robots. These figures do not indicate a passing fad, but rather a shift in the technical architecture of internal transport. Companies are investing more selectively, increasingly favoring modular, software-driven, and incrementally expandable solutions.
For Fluro, this means a favorable, but not risk-free, environment. The technology is established enough not to be considered experimental. At the same time, the supplier market is changing rapidly. Interfaces, fleet management systems, and safety concepts are constantly evolving, while Asian manufacturers account for a large share of the world's mobile robot production. Therefore, long-term integration capability is becoming increasingly important for operators. The purchase price of a vehicle is no longer the only deciding factor; rather, it's crucial that spare parts, software maintenance, interfaces, and competent service remain available throughout the robot's lifecycle.
Your intralogistics experts
Consulting, planning and implementation of complete solutions for high-bay warehouses and automated storage systems - Image: Xpert.Digital
More information here:
Innovative approaches in intralogistics for medium-sized businesses
Economic efficiency begins with avoiding complexity
A sound investment analysis must not reduce the benefits to saved working hours. While mobile robots can handle recurring transport tasks and relieve employees of unproductive walking and driving, the greater leverage often lies in more stable processes. When materials arrive on time and are traceable, search efforts, waiting times, and spontaneous interruptions decrease. Machines can be supplied more consistently, orders processed more reliably, and inventory managed more accurately. These effects are distributed across multiple cost centers and are easily underestimated in simple amortization calculations.
On the cost side, in addition to vehicles and warehouse technology, integration, software, structural modifications, safety measures, training, maintenance, spare parts, energy, and project management must also be considered. Furthermore, start-up losses during the ramp-up phase must be factored in. Automated systems rarely reach their planned performance on the first day of operation. Processes need to be readjusted, master data corrected, and employees trained to handle exceptions. A sound calculation therefore incorporates several scenarios: a cautious ramp-up, a realistic regular operation, and a growth scenario.
Land value is another economic factor. Stationary conveyor technology, wide transport routes, and decentralized intermediate storage areas require space that could alternatively be used for value-adding production. After the new facility is operational, the existing warehouse can be dismantled; the freed-up space can then be used for further production expansions. This effect significantly alters the investment logic. The new logistics system not only generates its own output but also frees up productive space elsewhere. Its benefits therefore also include the avoided costs of an additional production building or space constraints.
Capital commitment impacts delivery capability
Warehouse automation is often equated with inventory reduction. However, an automated warehouse doesn't automatically reduce inventory. Rather, it creates better conditions for transparent inventory management and more nuanced control. Whether less capital is actually tied up depends on planning parameters, delivery times, service targets, and demand uncertainty. For critical components, a higher safety stock may be more economically advantageous than a tight, unreliable supply.
For a provider of standard and custom solutions, striking this balance is particularly challenging. High delivery readiness can be a crucial competitive advantage, as customers often require spare parts or precision components at short notice. Simultaneously, a broad product range ties up capital and warehouse space. The new system can help manage fast-moving and slow-moving items differently, analyze access frequencies, and align inventory more closely with actual consumption patterns. Slow-moving items don't necessarily need to be eliminated if they secure strategically important customer relationships. However, they should be managed carefully and their true costs evaluated.
Linking ERP, warehouse management, and automated technology also creates a better data basis for inventory decisions. A prerequisite is that the book inventory and the physical inventory match. Inventory discrepancies, unrecorded withdrawals, or incorrectly assigned containers can severely disrupt automated processes. Therefore, inventory accuracy is not a minor administrative issue, but a key operational performance indicator. The higher the degree of automation, the less room there is for informal corrections by experienced employees.
Productivity without personnel illusions
Automation is often prematurely portrayed as the answer to labor shortages. While Germany continues to have numerous shortage occupations, there is no general labor shortage in every profession and region. At the same time, warehouse logistics faces significant staffing and matching problems. Therefore, the impact on personnel in Fluro should be viewed objectively. Five mobile robots don't simply replace five people. They take over defined transport tasks, while employees continue to provide materials, pick orders, ensure quality, process exceptions, monitor equipment, and improve processes.
The key advantage lies in a different use of limited working time. Qualified employees should spend as little time as possible on monotonous tasks when their knowledge generates greater value in manufacturing, quality control, or order processing. At the same time, new demands arise. Operators must understand system states, classify malfunctions, and be able to work with digital interfaces. Maintenance and IT require expertise at the intersection of mechanics, sensors, wireless technology, and software. The workplace doesn't automatically become easier; in many cases, it becomes more demanding and more data-driven.
Acceptance is therefore not achieved through the announcement of modern technology, but through participation. Employees are familiar with bottlenecks, special cases, and pragmatic solutions that are missing from process diagrams. Incorporating this experience early on improves not only acceptance but also plant design. Ignoring it risks automating a theoretically sound but practically cumbersome process. Training must begin before ramp-up and cover specific roles: daily operation, troubleshooting, approvals, maintenance, data management, and continuous improvement.
Safety is part of the service
Autonomous mobile robots operate in areas where humans, forklifts, and other vehicles may also be present. Therefore, safety is not an add-on feature but an integral part of the operational concept. DIN EN ISO 3691-4 specifies safety requirements and procedures for verifying driverless industrial trucks and their systems. Key factors include person detection, safe stopping functions, speed, load status, operating modes, and the design of the operating environment.
A technically safe vehicle alone does not constitute a safe overall system. Intersections, gates, areas with poor visibility, transfer stations, and shared traffic routes must be considered in the risk assessment. Employee behavior also plays a role. If time pressure leads people to enter transfer zones, improperly place loads, or disregard traffic rules, even good sensor systems become ineffective. Therefore, safety design and process design must be approached together.
Safety also impacts productivity. Overly cautious safety zones or unfavorable encounter areas can frequently slow down vehicles and reduce throughput. Conversely, overly aggressive settings increase risk. The optimal solution separates traffic types where economically viable and designs unavoidable mixed areas clearly and predictably. Regular inspections, clean sensor surfaces, controlled software updates, and reassessments after layout adjustments are all part of the lifecycle. Flexibility doesn't mean arbitrarily altering routes, but rather implementing changes in a controlled, documented, and safe manner.
Cyber risks are driving along with
With every connected vehicle, the digital attack surface grows. Mobile robots communicate via wireless networks, access orders, and interact with warehouse technology, gates, stations, and other systems. The warehouse management system is connected to the ERP system, thus forming a bridge between operational technology and corporate IT. A failure doesn't have to result from a spectacular attack; even faulty updates, expired certificates, network disruptions, or incorrectly configured access rights can disrupt the flow of materials.
A robust concept separates networks, restricts permissions, logs changes, and defines responsibilities for software versions. Restart plans are equally important. Fluro needs to know how production and shipping can continue in the event of a failure, which transport operations can be handled manually, and how long critical areas can remain functional without central control. Emergency procedures shouldn't be invented only after a disruption occurs.
Dependence on individual suppliers must also be considered. Proprietary interfaces can simplify integration, but may also bind the operator to specific software or vehicles in the long term. Open, documented interfaces and clear data access regulations increase strategic flexibility. Complete vendor independence is hardly realistic in complex systems. The crucial point is to understand dependencies, structure them contractually, and limit them technically where they could impair future competition or scalability.
Energy efficiency is more than just electricity consumption
Mobile robots require energy, charging infrastructure, and batteries. However, their direct electricity consumption is only one aspect of the ecological and economic assessment. The overall system impact is what matters. Shorter distances, fewer empty trips, more compact storage, and improved production supply can save energy and space. At the same time, additional hardware, batteries, servers, and automated warehouse technology also generate their own resource consumption. A sound assessment therefore avoids simplistic sustainability claims.
From an operational perspective, energy management that links charging cycles to order volume is beneficial. Vehicles can use short breaks for intermediate charging or charge specifically during off-peak hours. This reduces downtime but must not unnecessarily accelerate battery aging. Peak loads in the building should also be considered, especially when machinery, warehouse equipment, and other electrical consumers are operating simultaneously. While the five vehicles are not the site's largest energy consumers, their charging management can be organized as part of a broader digital energy system.
Another sustainability benefit lies in the system's lifespan. Modular and reconfigurable systems can remain usable for longer periods when processes change. A conveyor system that requires costly rebuilding or dismantling after just a few years loses some of its initial efficiency. Mobile robots are easier to relocate, expand, or use for other tasks. However, this advantage requires long-term maintenance of software, batteries, spare parts, and interfaces. Technical flexibility without a lifecycle strategy remains just that—a promise.
The ramp-up determines the return
The planned start of operations in December 2027 allows sufficient time for planning, construction, integration, and testing, but also increases the risk that assumptions may change by then. Quantities, product mix, shift patterns, or production layouts can all shift within such a timeframe. Therefore, project management should not only pursue a static target state but also regularly review key planning parameters. Particularly relevant are transport volumes, peak load profiles, product structure, container types, and the location of future machinery.
Realistic testing is required before live operation. This includes normal operation, peak load, individual vehicle failures, blocked routes, empty transfer points, incorrect load carriers, and restarting after IT or power outages. An acceptance test that only demonstrates trouble-free standard procedures says little about everyday usability. Equally important is a sufficiently long stabilization phase after startup. During this time, key performance indicators should be closely monitored, problems prioritized, and changes implemented in a controlled manner.
A phased rollout can reduce risks. Clearly defined transport relationships can be activated first, before complex priority logics and additional variants are introduced. This allows employees and technology to learn together. However, a gradual ramp-up must not result in a permanent temporary solution. Each stage requires measurable criteria and a binding transition to the next level of maturity. The return on investment only materializes when the planned scope of automation is consistently utilized and manual parallel processes are actually phased out.
Key performance indicators must measure the overall flow
Controlling the new system requires key performance indicators (KPIs) that go beyond the availability of individual machines. High technical availability of the robots is worthless if transfer stations are blocked or the warehouse provides the wrong containers. Conversely, a single malfunction may be inconsequential if the fleet compensates for it and production is supplied on time. What matters is performance from the perspective of the overall process.
Suitable metrics include on-time production supply, average and maximum transport throughput time, the number of late orders, the percentage of productive trips, the empty run rate, and the utilization of critical transfer points. Additional metrics include inventory accuracy, picking errors, manual interventions, downtime, and energy consumption per transport. Key performance indicators should be differentiated by shift, order type, and process area to ensure that average values do not mask bottlenecks.
The connection between technical and economic factors is particularly important. If transport times are reduced, it must be verified whether this actually leads to a decrease in machine downtime, inventory levels, or personnel requirements. If additional vehicles increase the service level, it must be assessed whether the benefits justify the capital and operating costs. This results in a continuous investment analysis rather than a one-time justification before the project begins. The system is thus not only operated but also systematically developed further.
Scaling needs clear boundaries
A mobile concept facilitates expansion, but scalability is not unlimited. Additional robots only increase transport capacity as long as traffic routes, transfer stations, and warehouse performance can keep pace. Beyond a certain point, each additional vehicle leads to more encounters, waiting times, and mutual obstruction. The fleet then grows numerically without generating a proportional increase in performance. Therefore, the initial layout should define where additional vehicles can be deployed and which bottlenecks need to be addressed beforehand.
The shuttle depot is also scalable, provided that structural, control-related, and financial prerequisites are taken into account. Reserves in parking spaces, capacity, and interfaces incur costs now but can significantly simplify future modifications. Conversely, overly generous reserves tie up capital for growth that may never materialize. A modular target model with clear triggers is advisable: If utilization consistently exceeds a defined value or peak load reaches a certain level, the next expansion stage is activated.
Fluro should avoid confusing flexibility with a lack of standardization. The more special containers, individual transfers, and differing rules exist, the more difficult scaling becomes. Standardized load carriers, clear interfaces, and reusable process modules create the foundation for quickly integrating new tasks. A flexible system is not one with the most exceptions, but rather one that manages changes with minimal standardized interventions.
SMEs can think differently about automation
The project has far-reaching implications beyond Fluro. Many medium-sized manufacturing companies face similar challenges: existing buildings, heterogeneous inventories, a high degree of product variety, limited space, and uncertain production volumes. Large, highly automated central warehouses are not always the right solution. They require significant initial investment and are only cost-effective with large, stable volumes. Modular combinations of automated storage, mobile transport, and integrated software may be a better fit for companies whose strength lies in specialization and adaptability.
The decisive success factor is not company size, but process maturity. A medium-sized company can automate highly effectively if material flows are understood, responsibilities are clearly defined, and master data is reliable. Conversely, even large projects fail if technology is imposed on unclear processes. Fluro is using the new building to combine spatial and organizational reorganization. This integration makes sense because the building, warehouse technology, and production supply can be planned together, instead of being optimized separately later.
At the same time, a sober perspective remains necessary. Five mobile robots neither solve every capacity problem nor automatically guarantee lower costs. The benefits depend on the quality of integration, operational discipline, and a willingness to continuously improve. Flexible technology does not forgive planning errors; it merely enables other corrections. Anyone who views automation as a one-off installation project is missing out on a significant portion of its potential.
Logistics is becoming strategic infrastructure
Fluro's new system demonstrates how the role of intralogistics is changing. Previously, it was often viewed as a support function, moving materials from one place to another as discreetly as possible. In a highly varied, time-critical production environment, it is becoming strategic infrastructure. It influences how quickly new products can be introduced, machines reconfigured, inventory levels adjusted, and customer orders prioritized. This directly impacts delivery capability, capital commitment, and growth rate.
The decision against a rigid conveyor technology approach should therefore not be interpreted as a blanket judgment on traditional technology. It is a response to the specific business model and the anticipated dynamics of change. Where fixed high-performance relationships exist, stationary systems remain superior. Where sources, sinks, and quantities change more frequently, mobile robotics can offer greater value. The combination with pallet and shuttle storage demonstrates that modern intralogistics rarely consists of a single technology. Crucially, it requires a suitable division of labor between high-performance warehouse automation and flexibly routable transport.
When Fluro combines technical components with clean data, clear standards, qualified employees, and consistent performance management, more than just a new warehouse is created. A platform for further production growth emerges. The economic benchmark is then no longer whether five robots impressively navigate a hall. What matters is whether the company can react faster, deliver more reliably, utilize space more productively, and manage future changes with less effort. This is precisely what will reveal whether flexible intralogistics is merely modern technology or a genuine competitive advantage.
Your global marketing and business development partner
☑️ Our business language is English or German
☑️ NEW: Correspondence in your native language!

Konrad Wolfenstein
I and my team are happy to be available to you as your personal advisor.
You can contact me by filling out the contact form here [email protected]:or simply call me at +49 7348 4088 965. My email address is
I'm looking forward to our joint project.